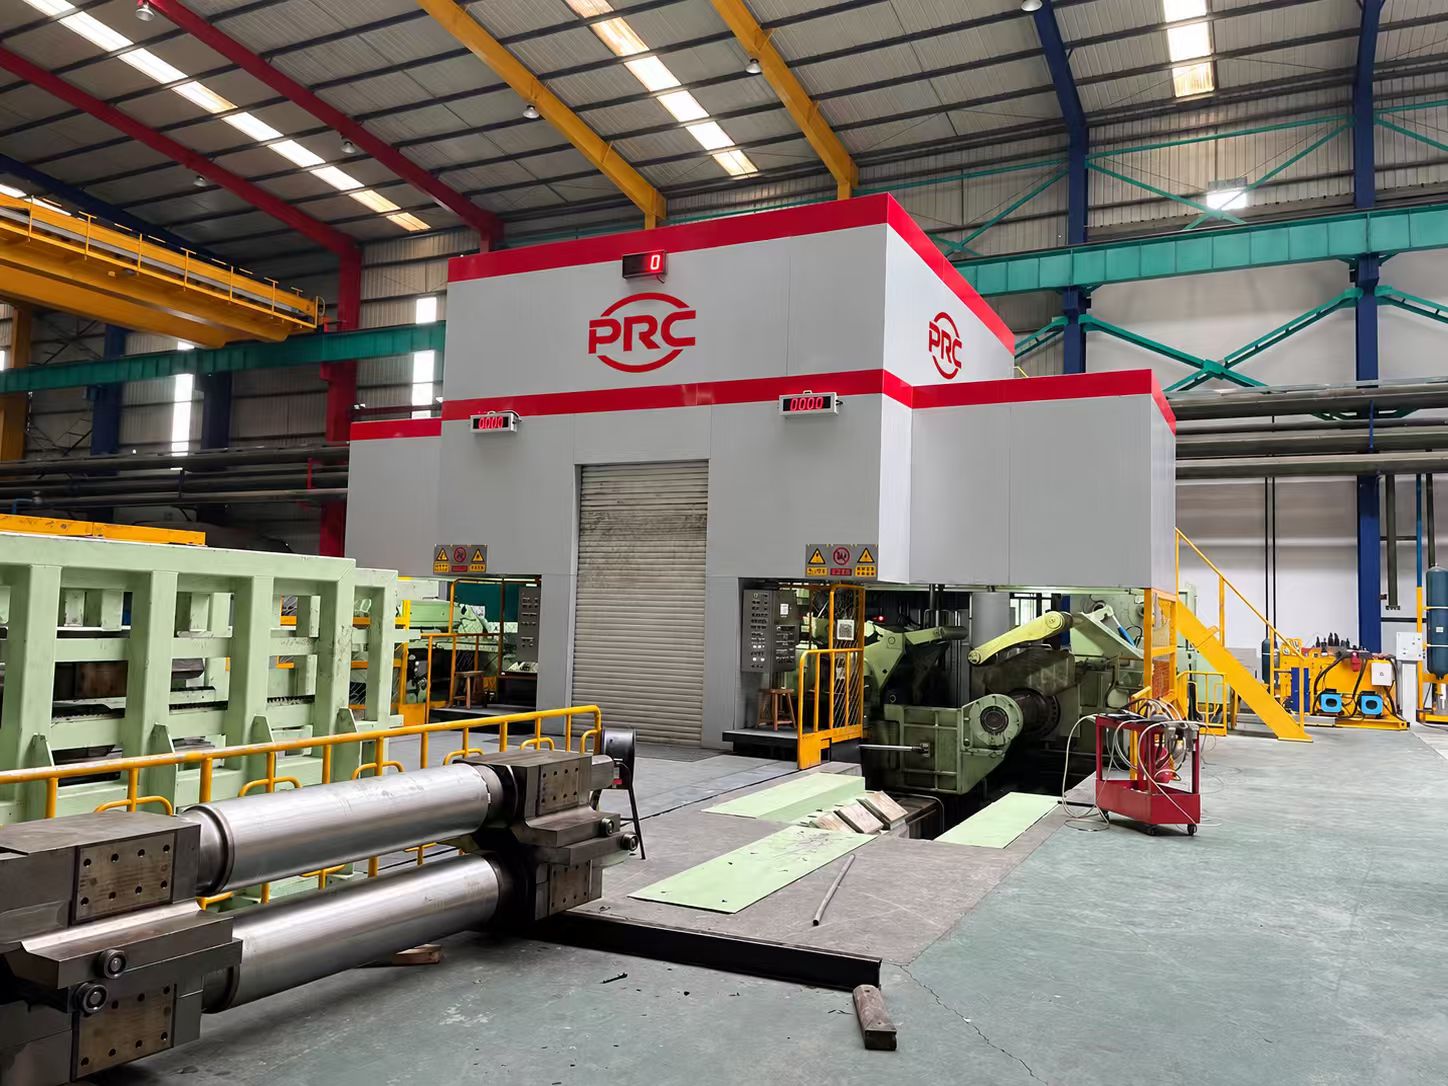
Strip Cold Rolling & Surface Treatment
Steel Strip Cold Rolling Mill (CRM)
Single- or two-stand reversing mills and four- to six-stand tandem mills, with selection data and a technical questionnaire.
View equipmentQuick enquiry questionnaire →
Select equipment by feedstock, finished product and processing task. Featured pages include materials, specification ranges, process configuration, site requirements and equipment photographs; search the complete catalogue below.
Single- or two-stand reversing mills and four- to six-stand tandem mills, with selection data and a technical questionnaire.
View equipmentQuick enquiry questionnaire →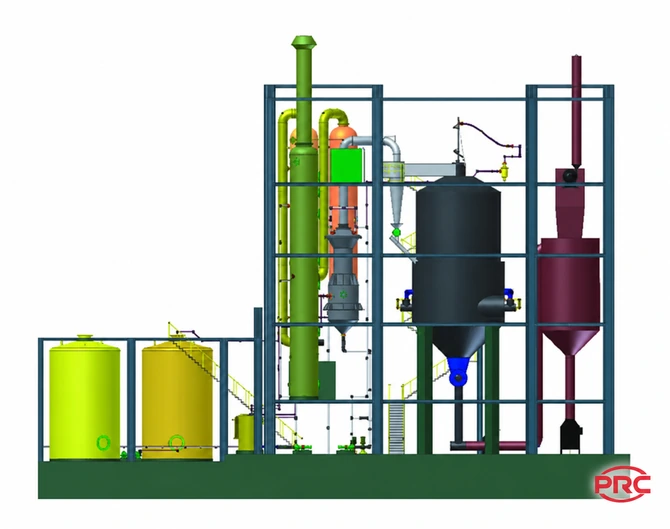
Acid regeneration for wasteacid, selected to suit the wasteacid composition.
View equipmentQuick enquiry questionnaire →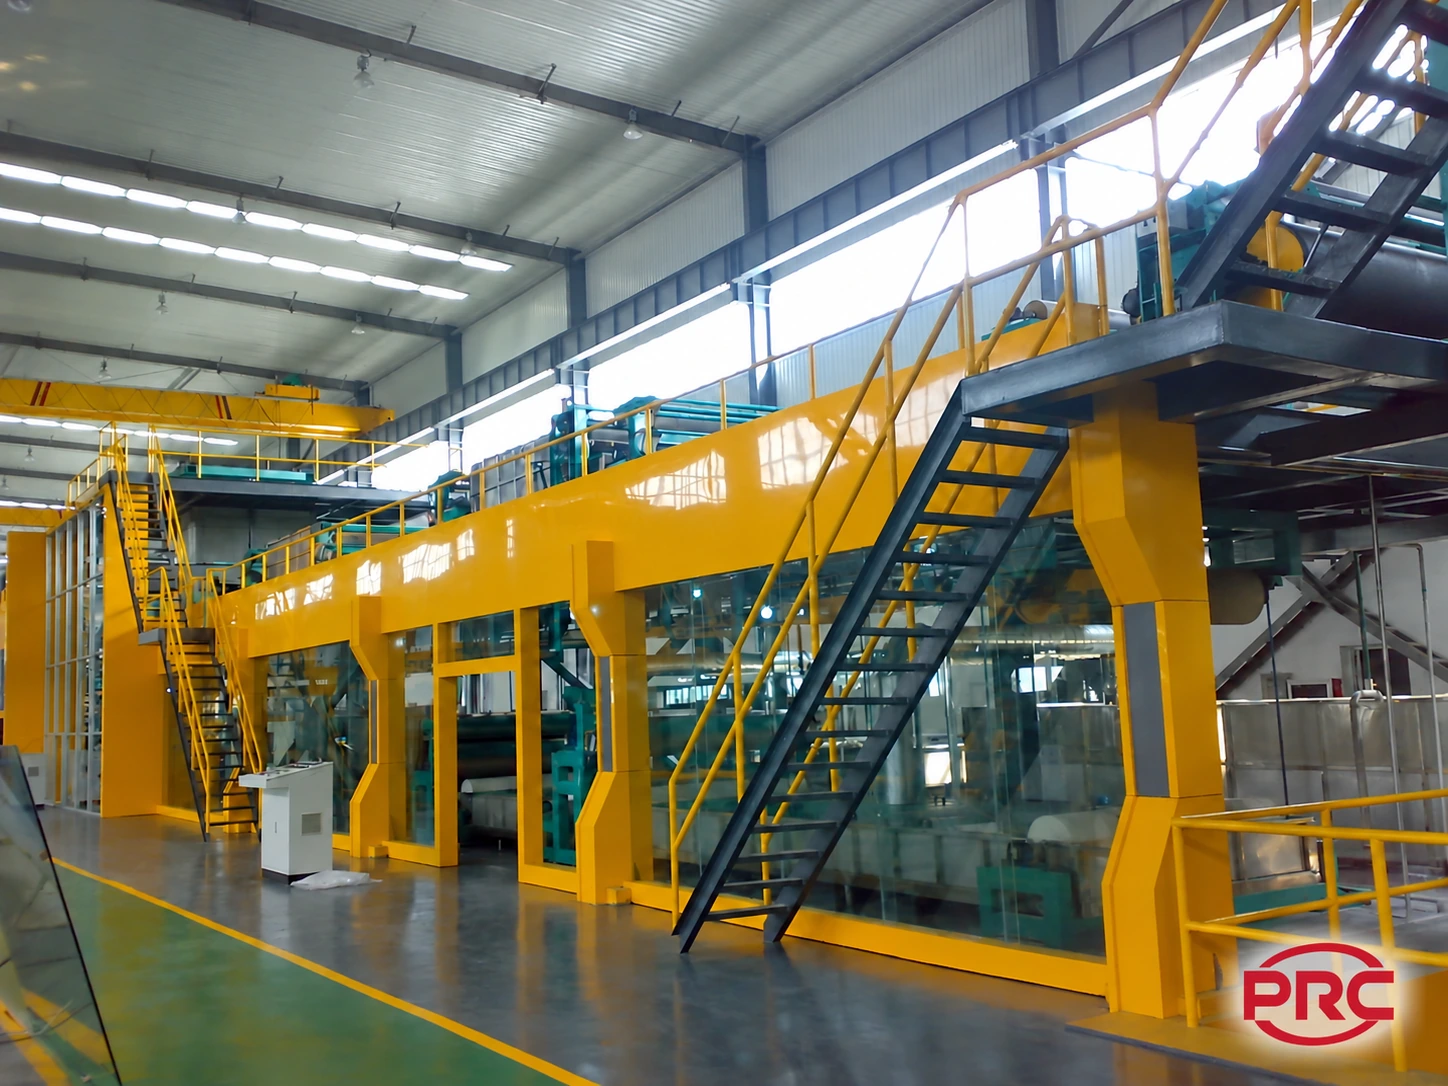
Continuous decorative and protective coating of cold-rolled or galvanized strip for building envelopes, appliances and industrial equipment.
Strip width 600–2000 mm · Strip thickness 0.18–1.6 mm
Surface preparation → Coating application → Baking / curing → Cooling & exit handling
Quick enquiry questionnaire →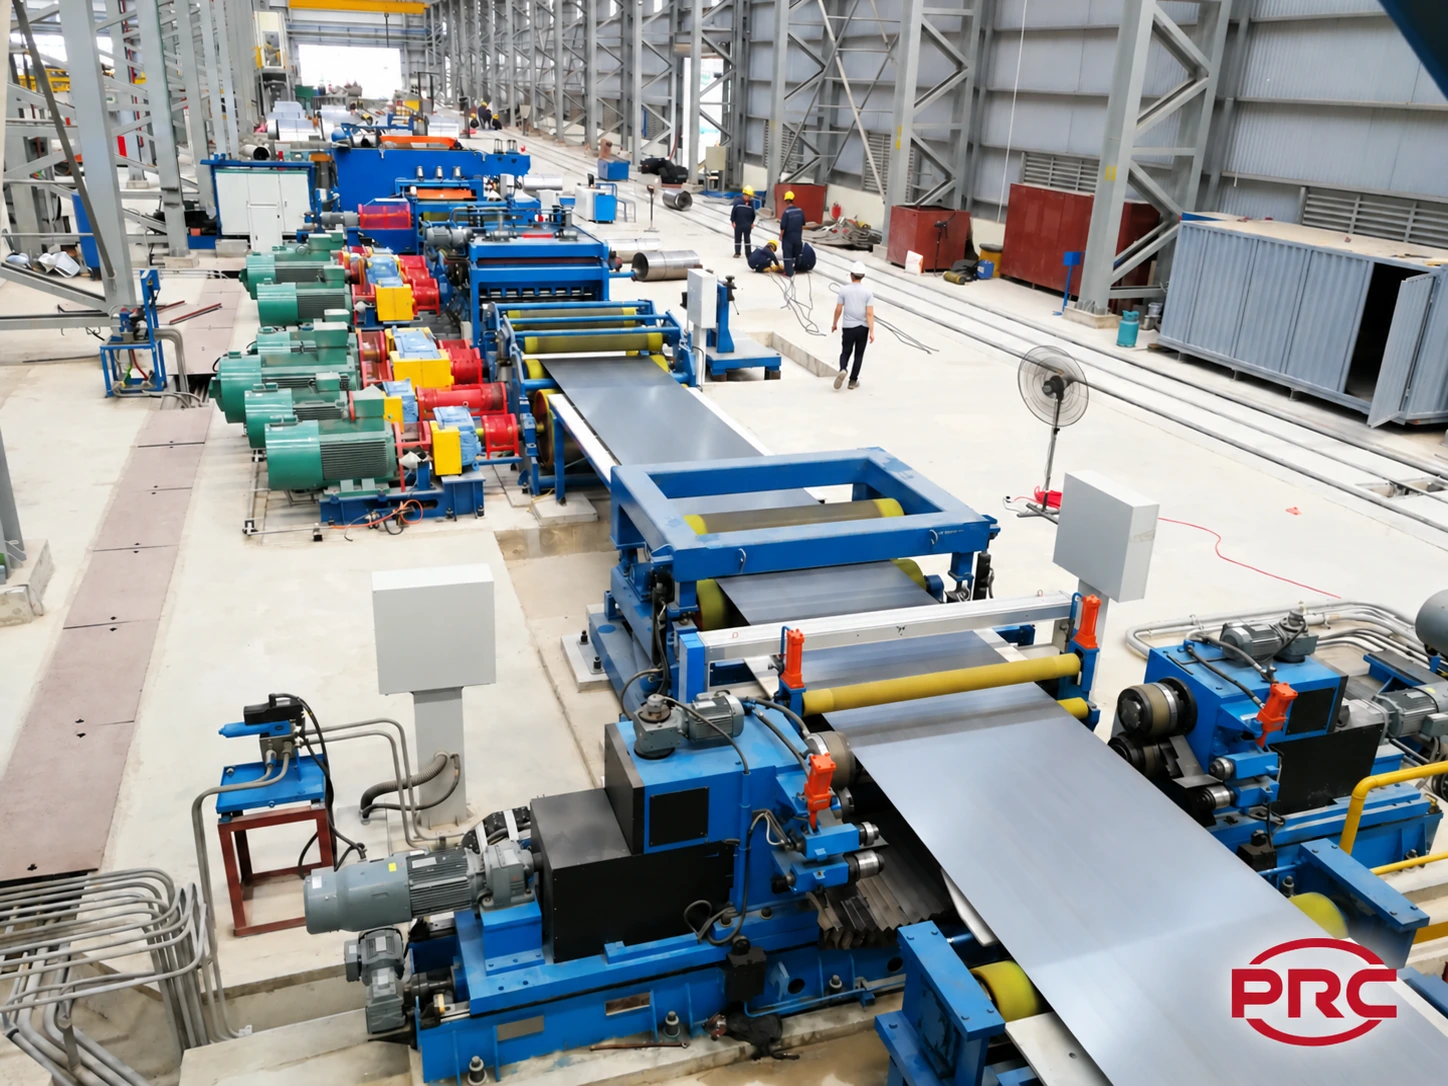
Strip tension leveling and finishing, including side trimming, oiling and recoiling configurations.
View equipmentQuick enquiry questionnaire →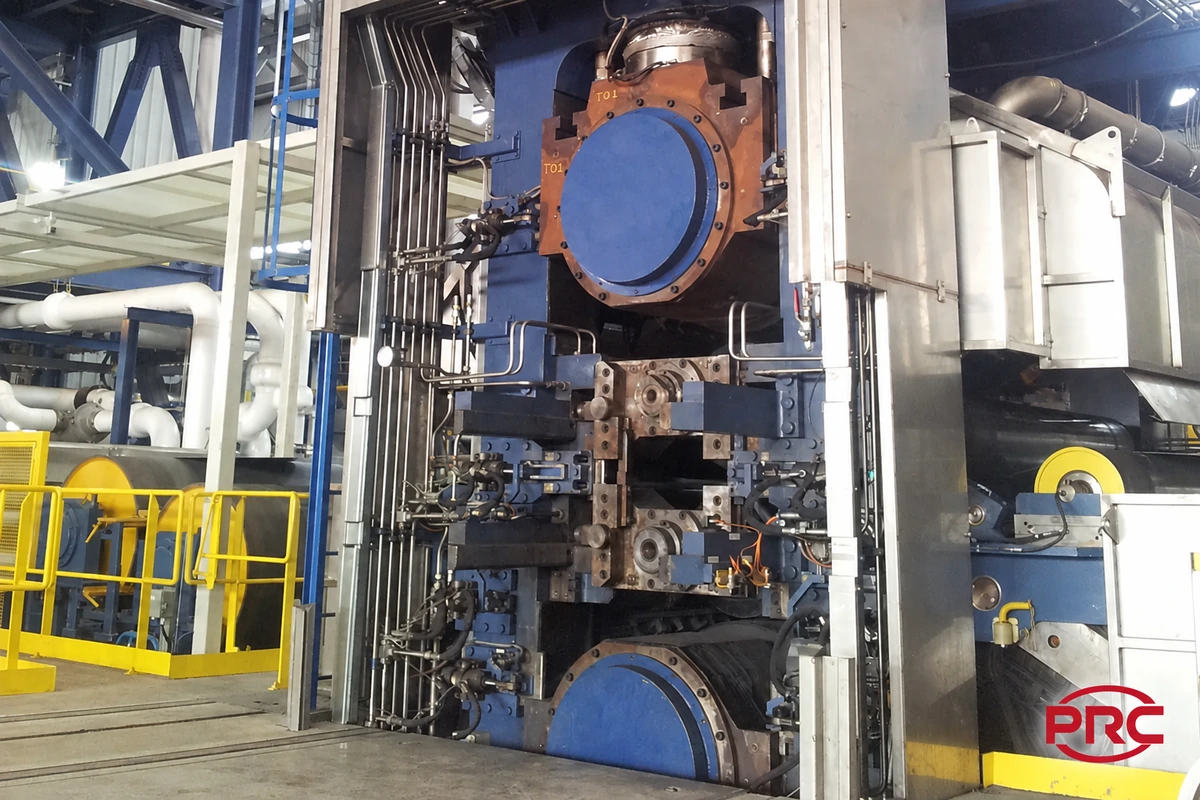
Four-high temper rolling for steel strip finishing.
View equipmentQuick enquiry questionnaire →Equipment type reference — not a PRC project photograph
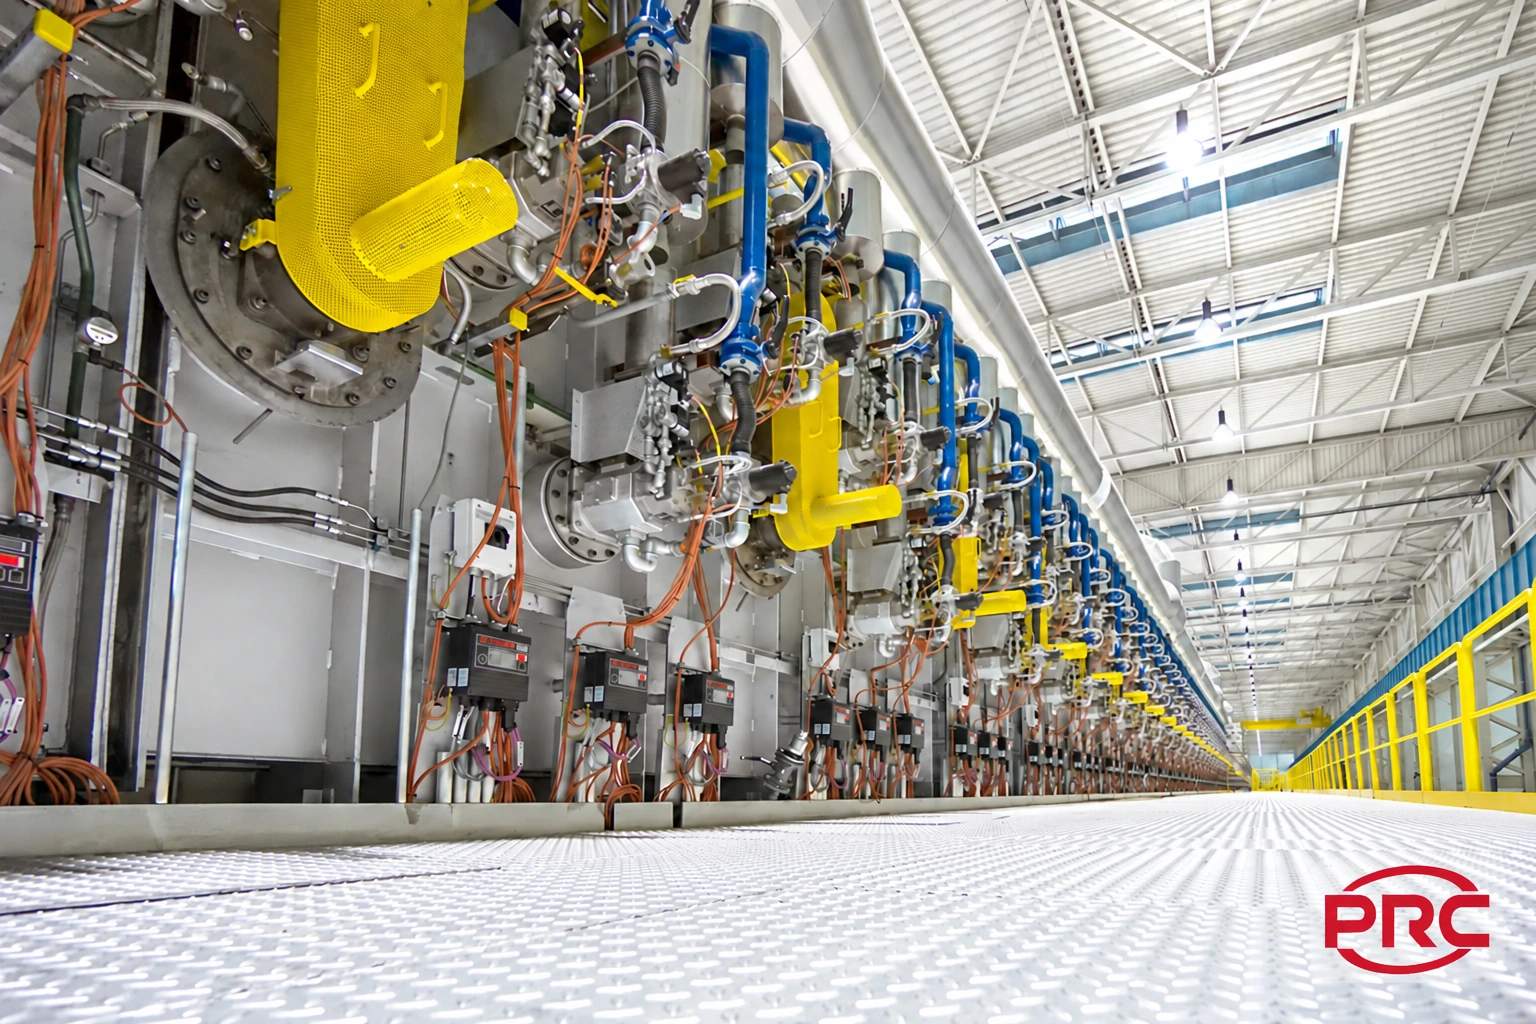
Annealing equipment for non-oriented electrical steel strip.
View equipmentQuick enquiry questionnaire →Equipment type reference — not a PRC project photograph
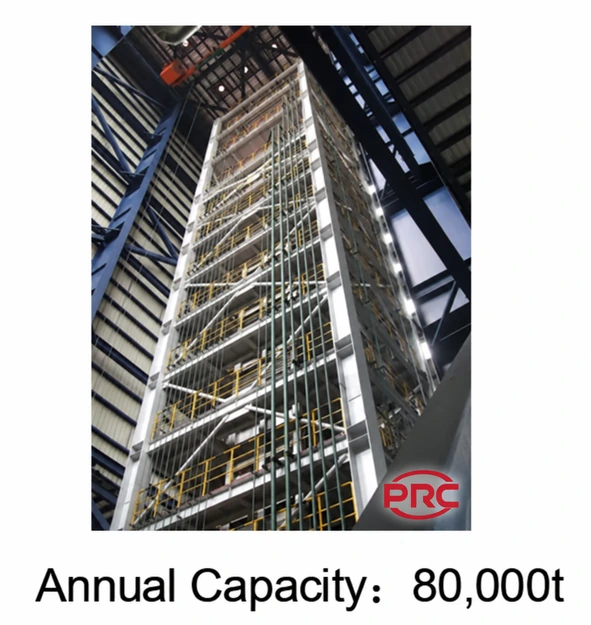
Continuous bright annealing equipment for stainless steel strip.
View equipmentQuick enquiry questionnaire →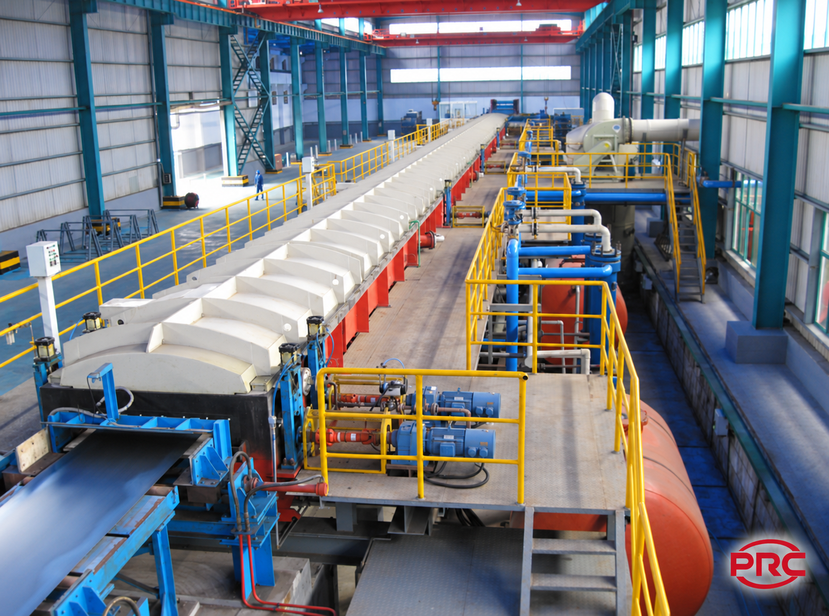
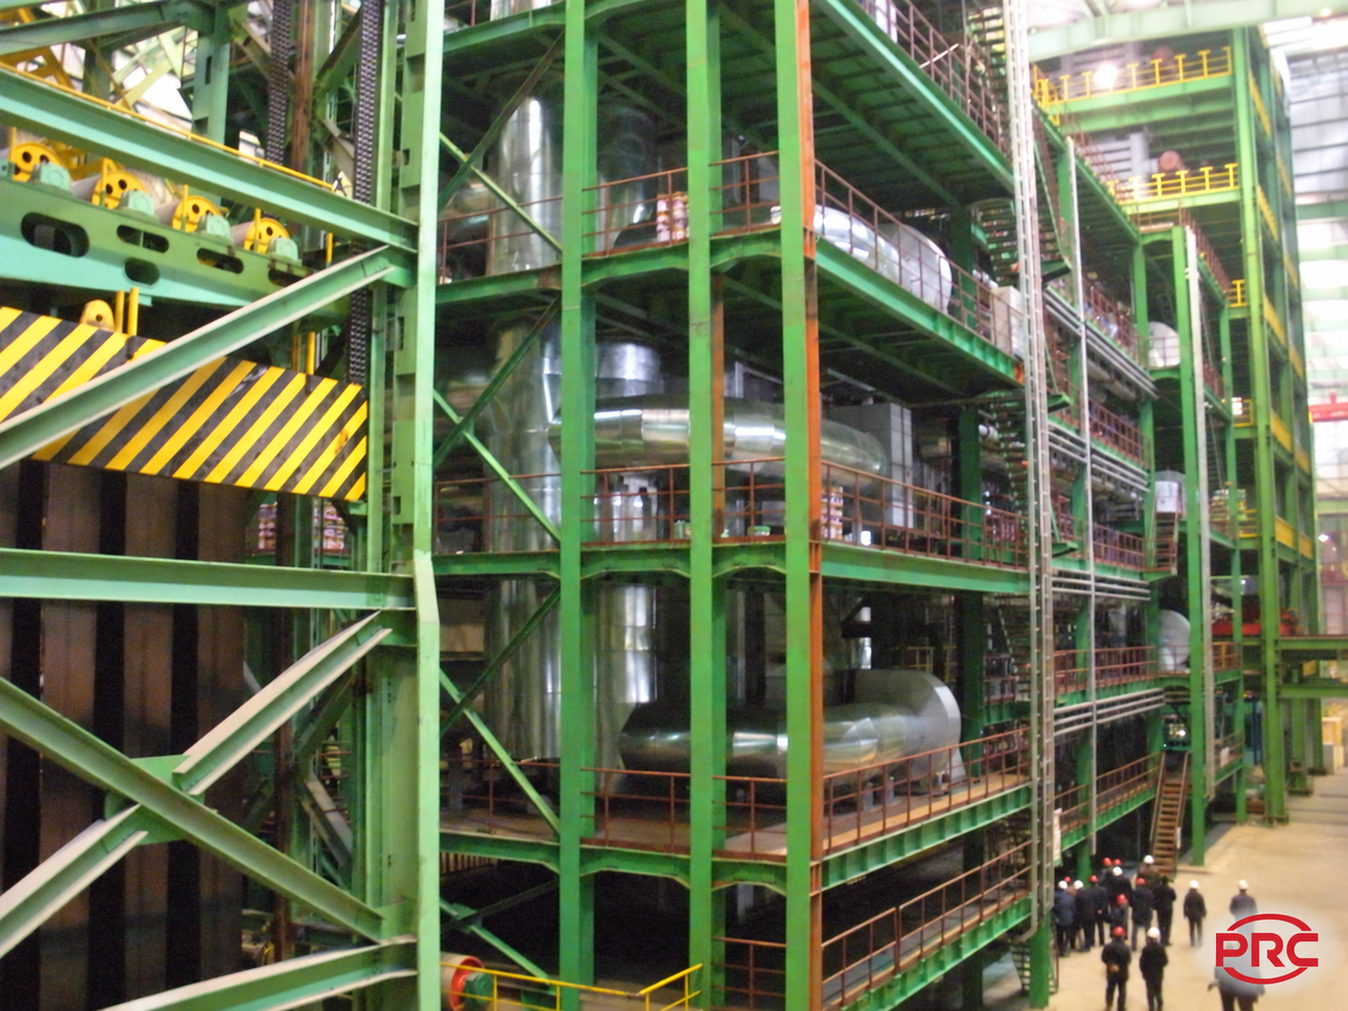
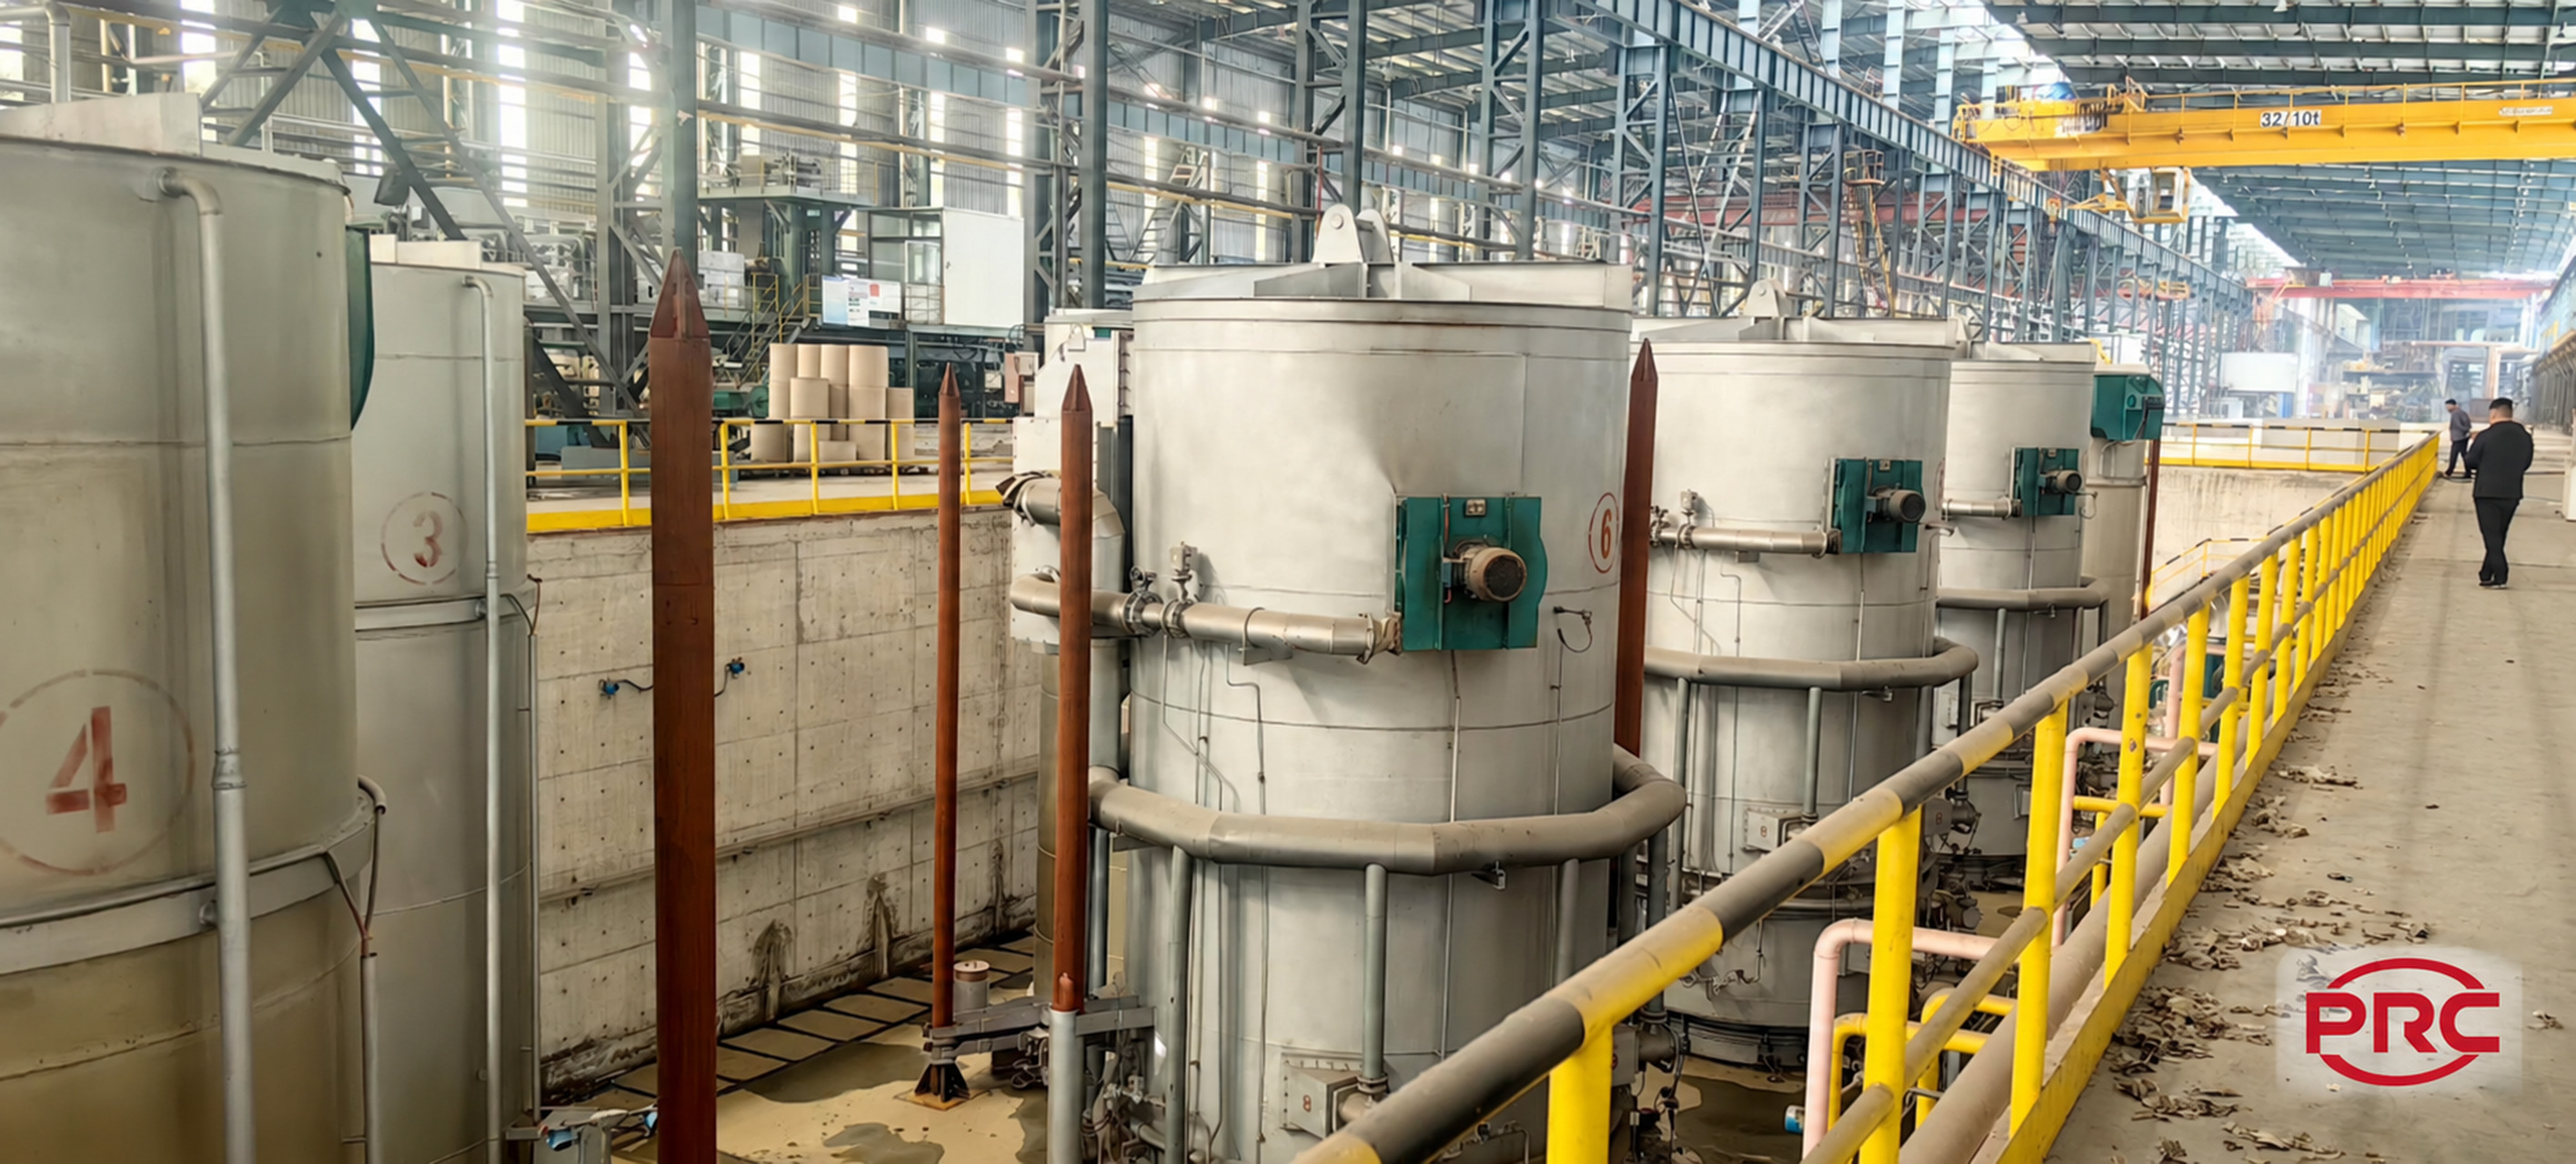
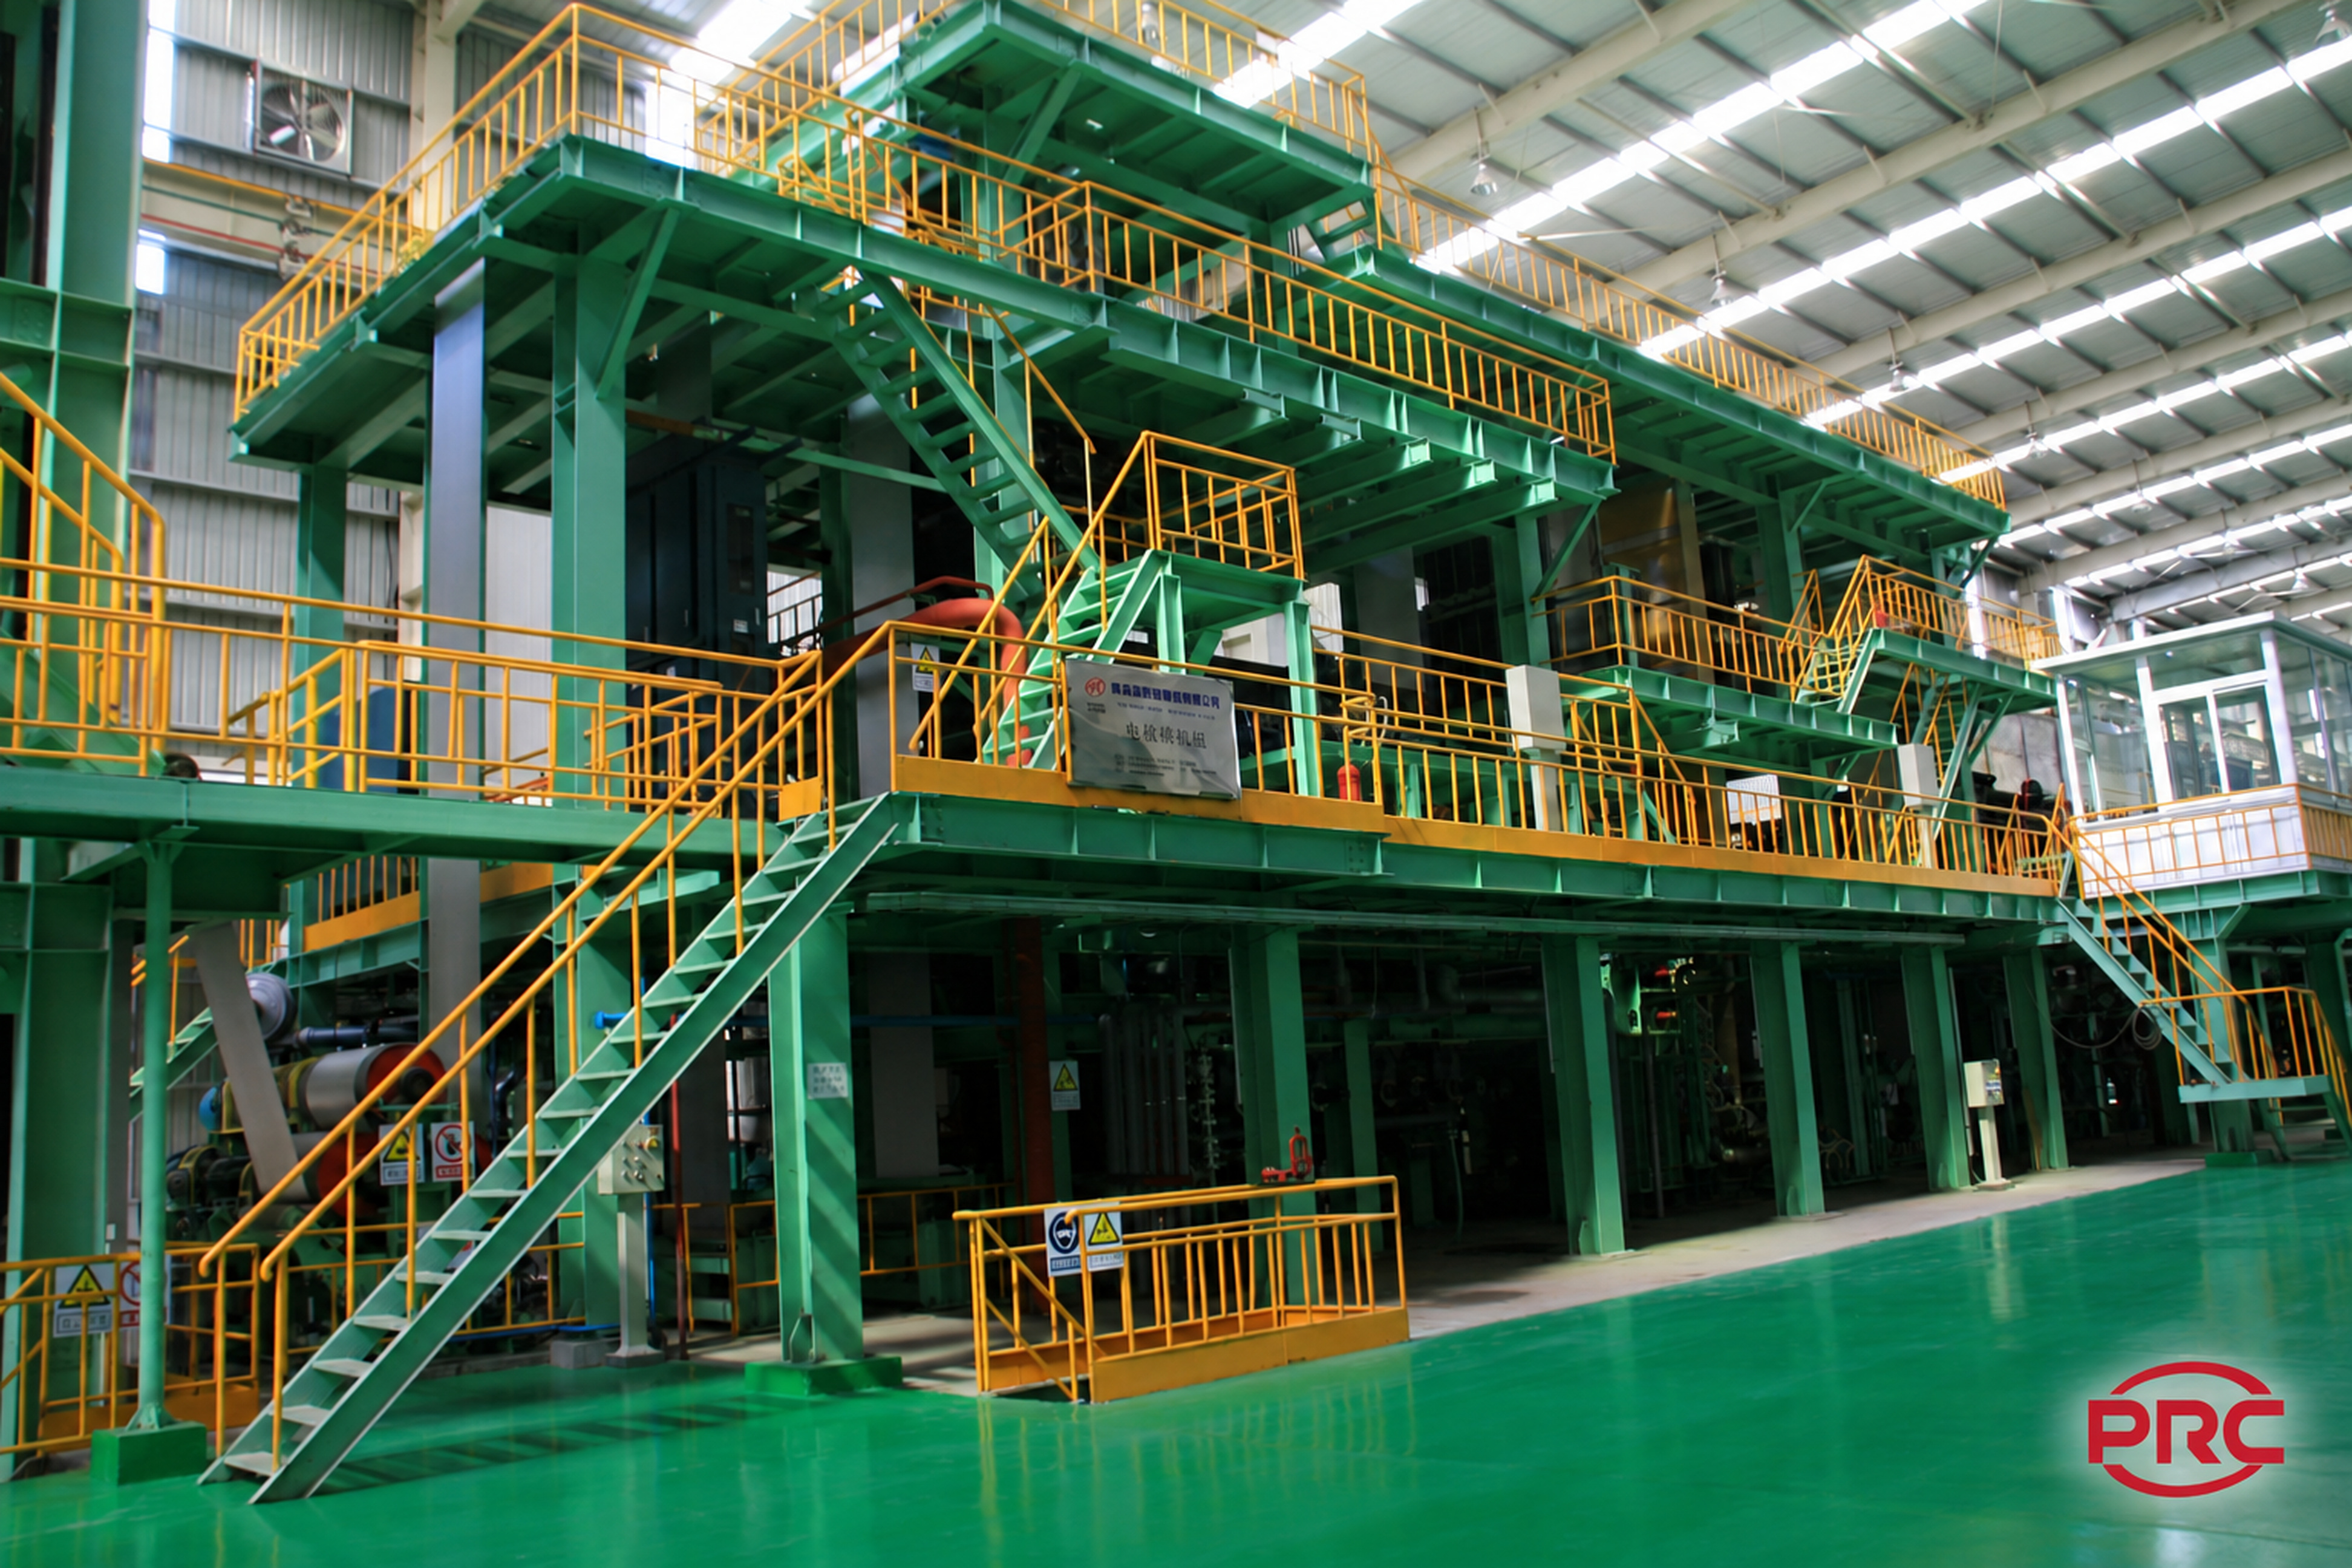
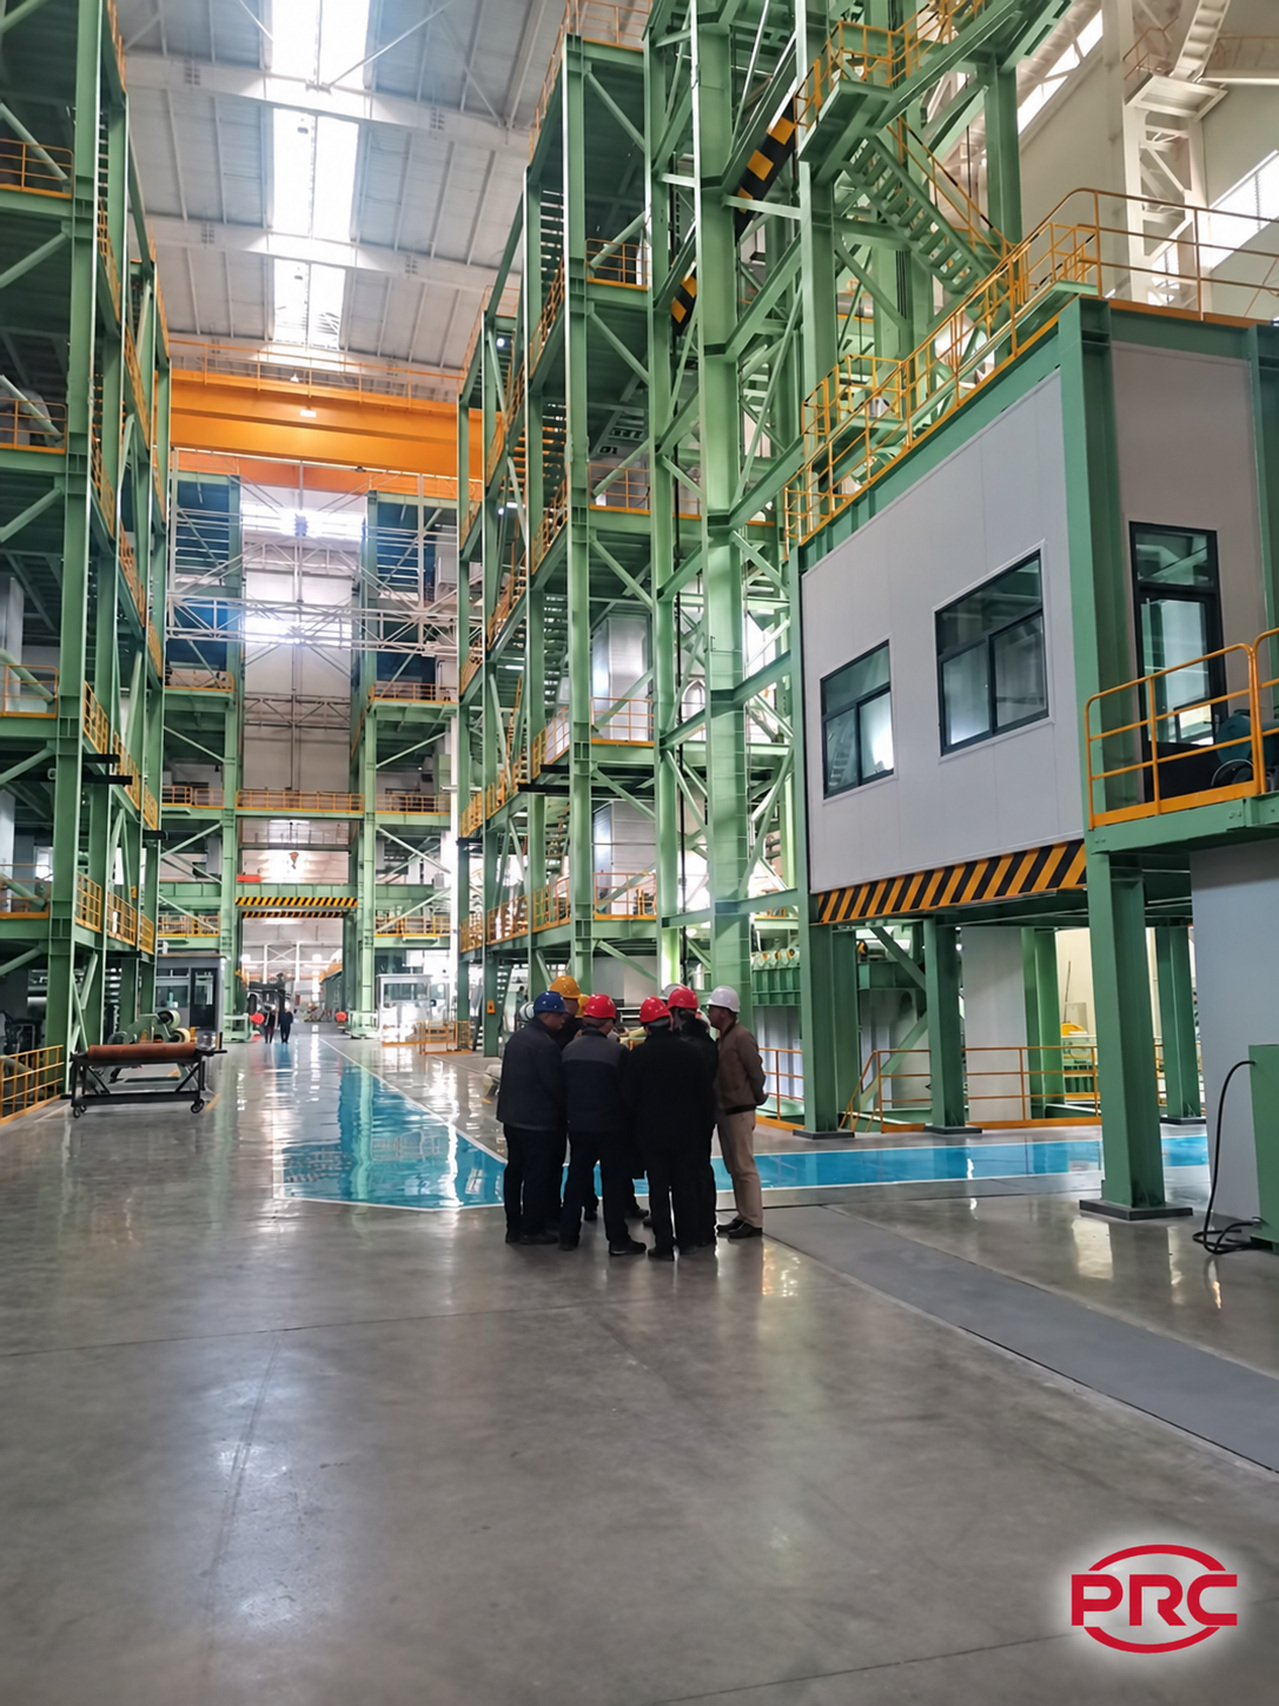
Continuous hot-dip and alloy coating of steel strip, covering cleaning, reducing annealing, coating, cooling, temper rolling and tension levelling. Galvanizing, galvalume and zinc-aluminium-magnesium coating require product-specific coating chemistry and equipment configuration.
Strip width 600–1800 mm · Strip thickness 0.15–6.0 mm
Cleaning & surface preparation → Reducing annealing → Hot-dip coating & coating control → Cooling → Temper rolling & tension levelling
Quick enquiry questionnaire →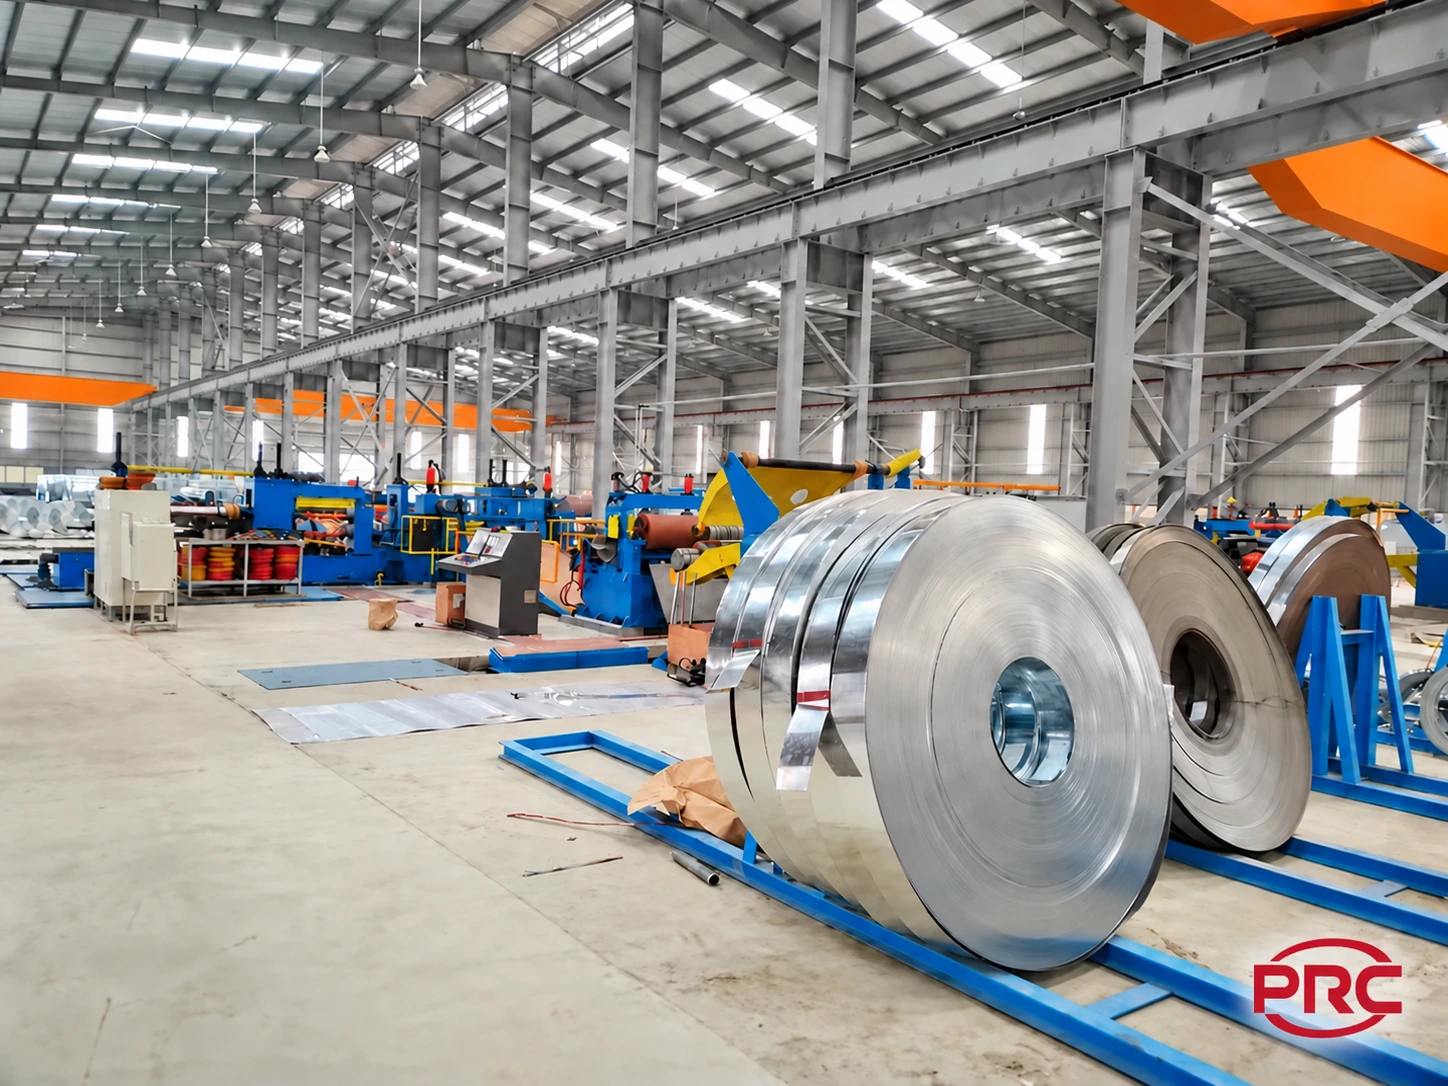
Uncoils wide metal coil, slits it longitudinally into narrow strips and recoils the strips for downstream tube making, forming and narrow-strip applications.
Material thickness 0.15–4.0 mm · Material width 300–2000 mm
Uncoiling → Rotary slitting → Strip recoiling
Quick enquiry questionnaire →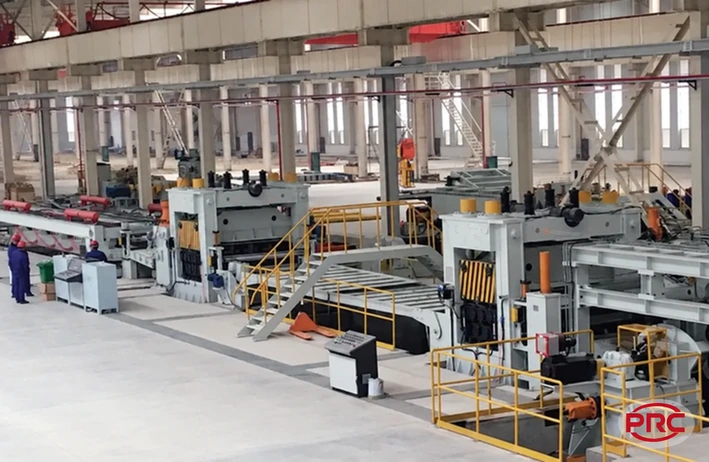
Uncoils, levels and transversely cuts metal coil into fixed-length sheets, then stacks the sheets for downstream processing.
Material thickness 0.5–4.0 mm · Material width 300–1800 mm
Uncoiling → Levelling → Shearing to length → Sheet stacking
Quick enquiry questionnaire →Recoiling and finishing of steel strip.
View equipmentQuick enquiry questionnaire →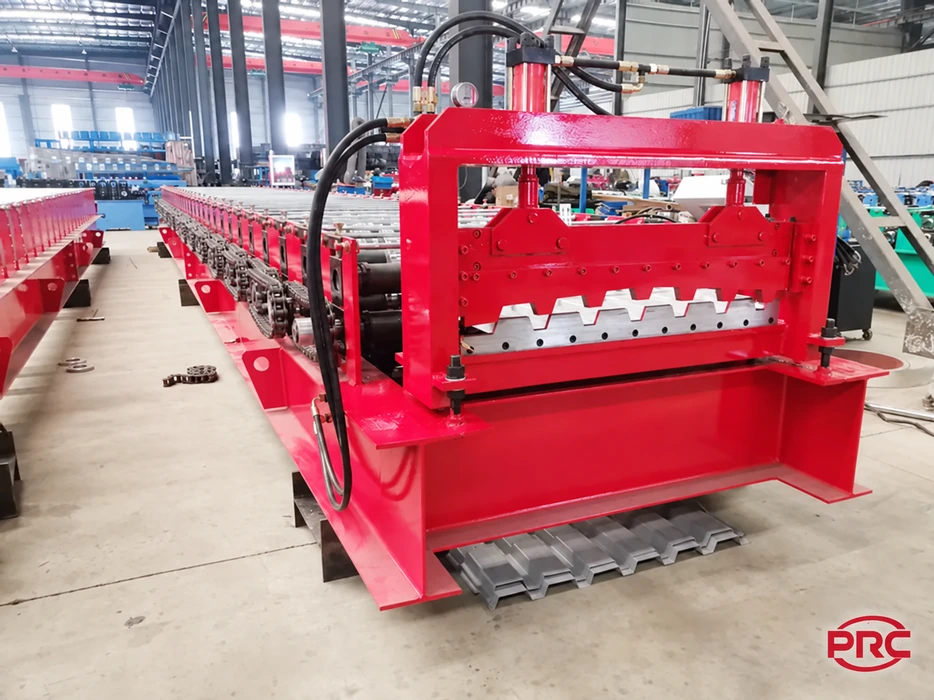
Roll forming of roofing and wall-cladding sheet profiles.
View equipmentQuick enquiry questionnaire →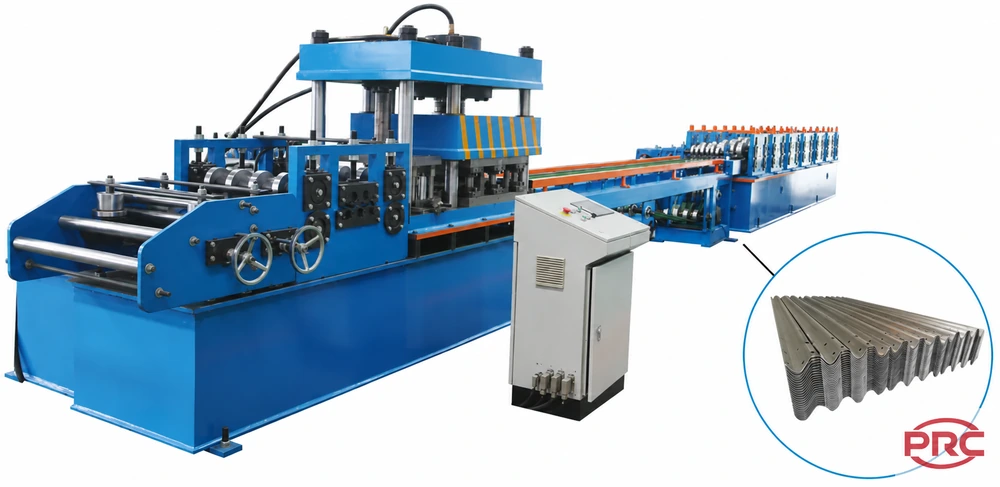
Roll forming for two-wave and three-wave highway guardrail profiles.
View equipmentQuick enquiry questionnaire →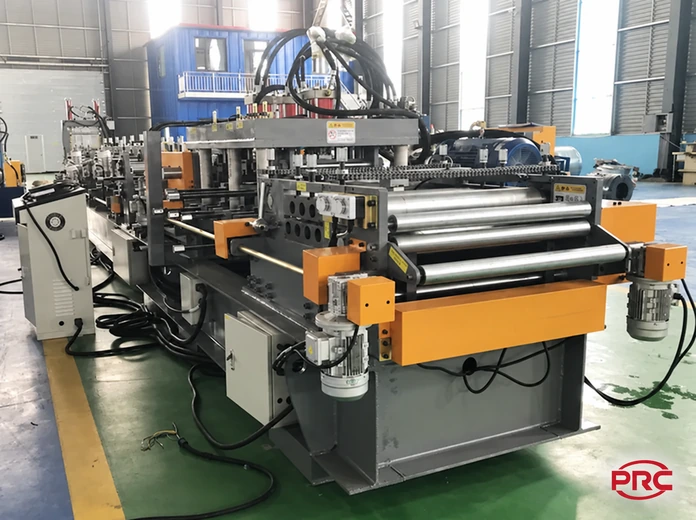
Cold roll forming of C, Z and U profiles from steel strip.
View equipmentQuick enquiry questionnaire →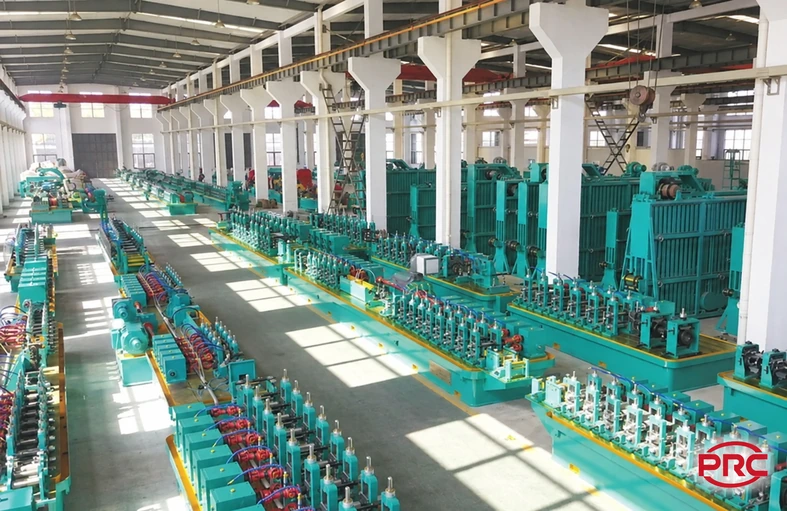
High-frequency welding converts hot-rolled, cold-rolled or galvanized strip into round, square and rectangular tubes for construction, transport, machinery and automotive applications.
Round tube diameter Ø7–Ø273 mm · Wall thickness 0.18–10 mm
Strip feeding → Roll forming → High-frequency welding → Cooling & sizing → Cut-to-length & discharge
Quick enquiry questionnaire →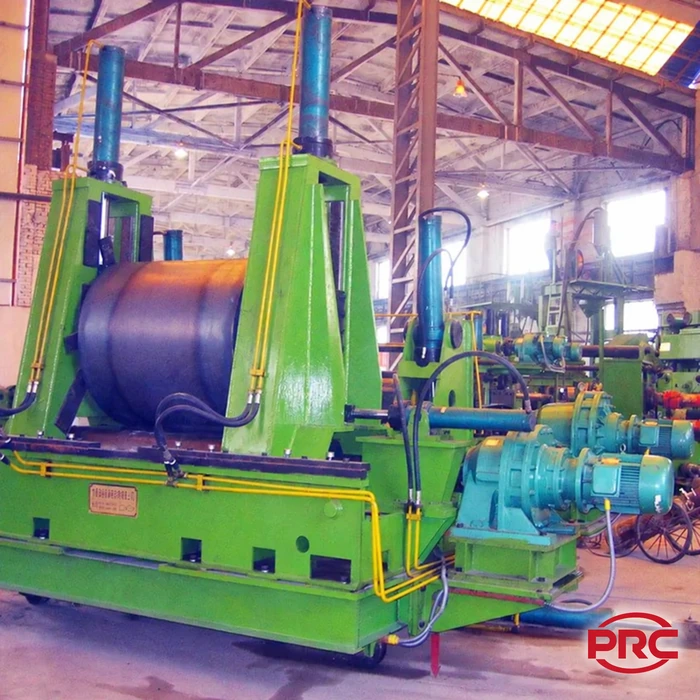
Spiral forming and submerged arc welding of steel pipe from coil.
View equipmentQuick enquiry questionnaire →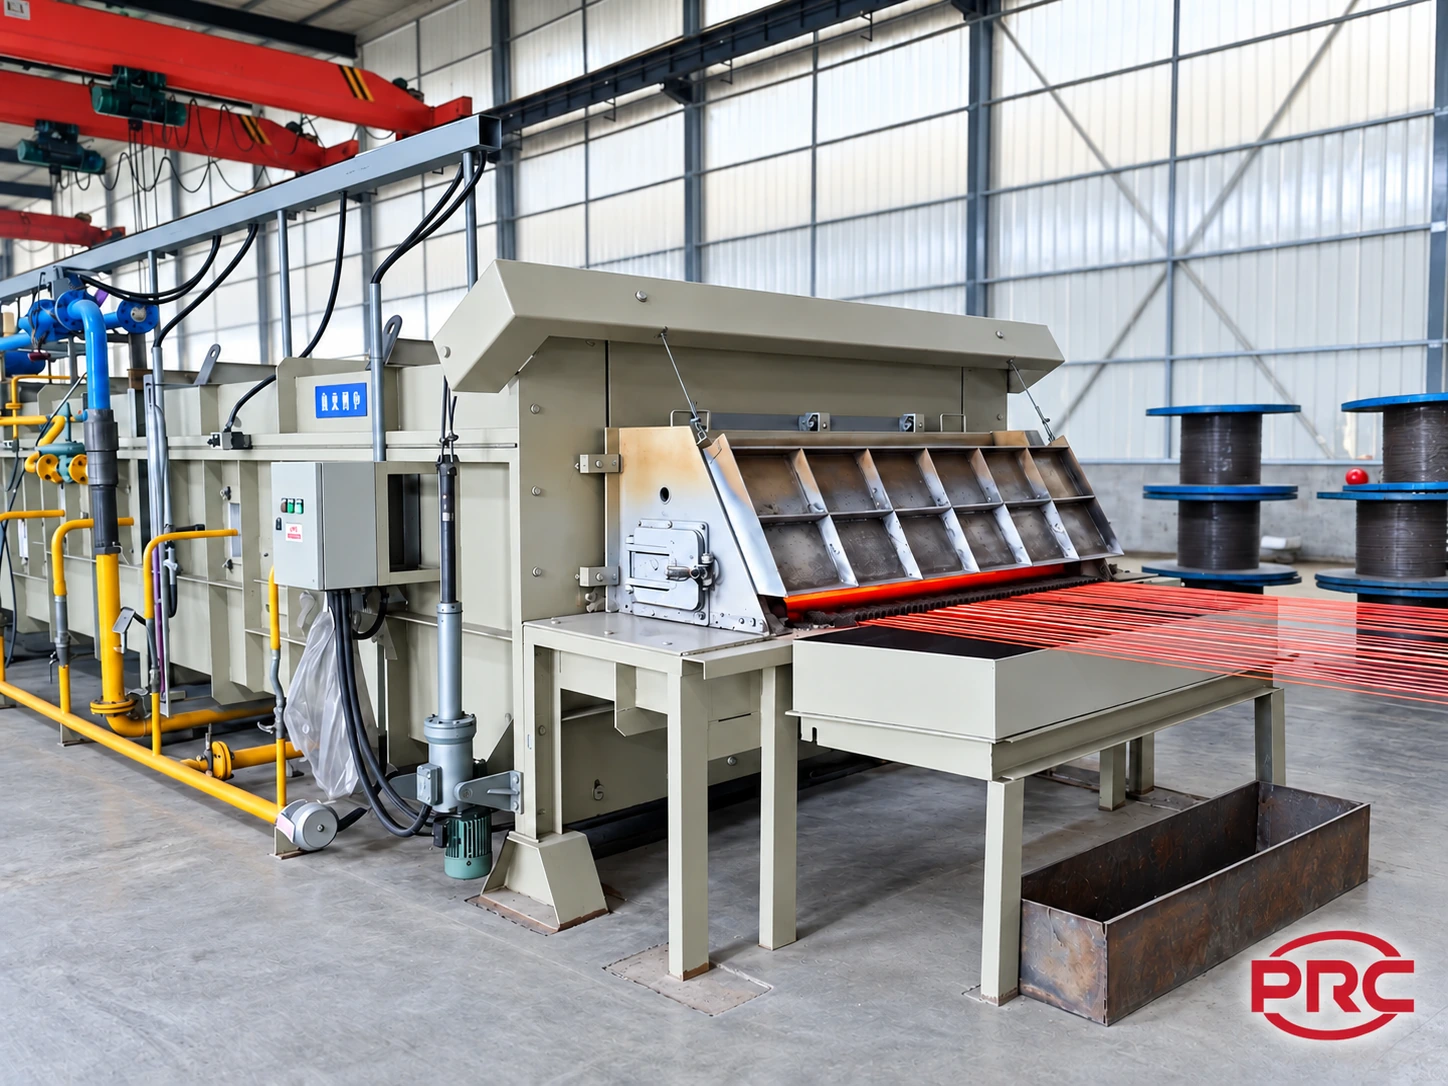
Pretreatment, zinc coating, cooling and post-treatment of steel wire.
View equipmentQuick enquiry questionnaire →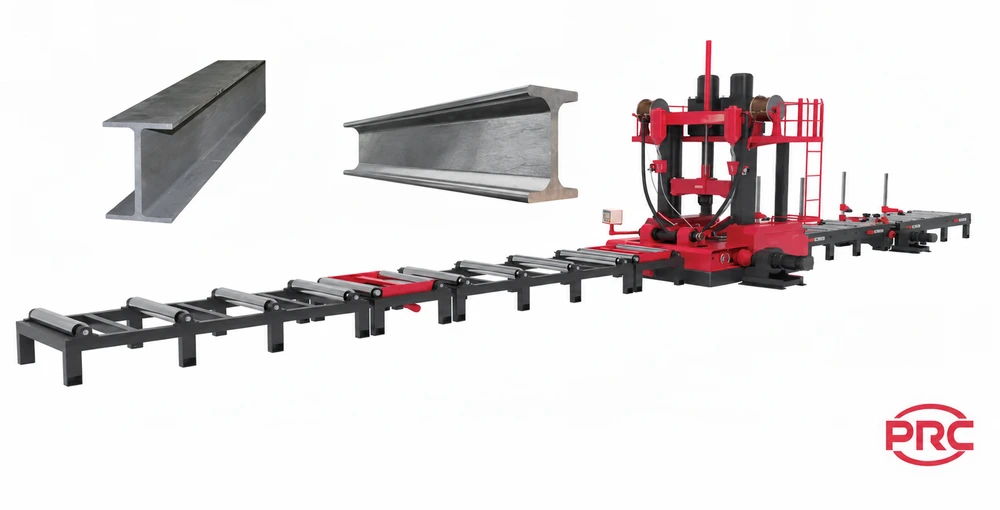
Submerged arc welding equipment for welded H-beam production.
View equipmentQuick enquiry questionnaire →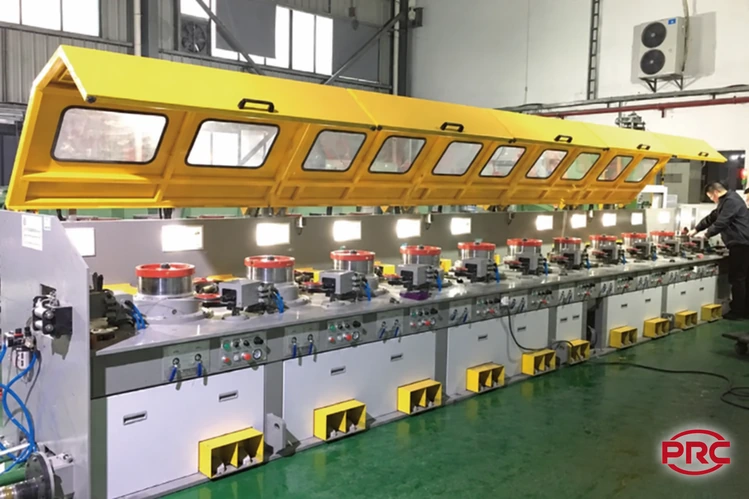
Wire diameter reduction through successive drawing dies, with feeding and take-up systems.
View equipmentQuick enquiry questionnaire →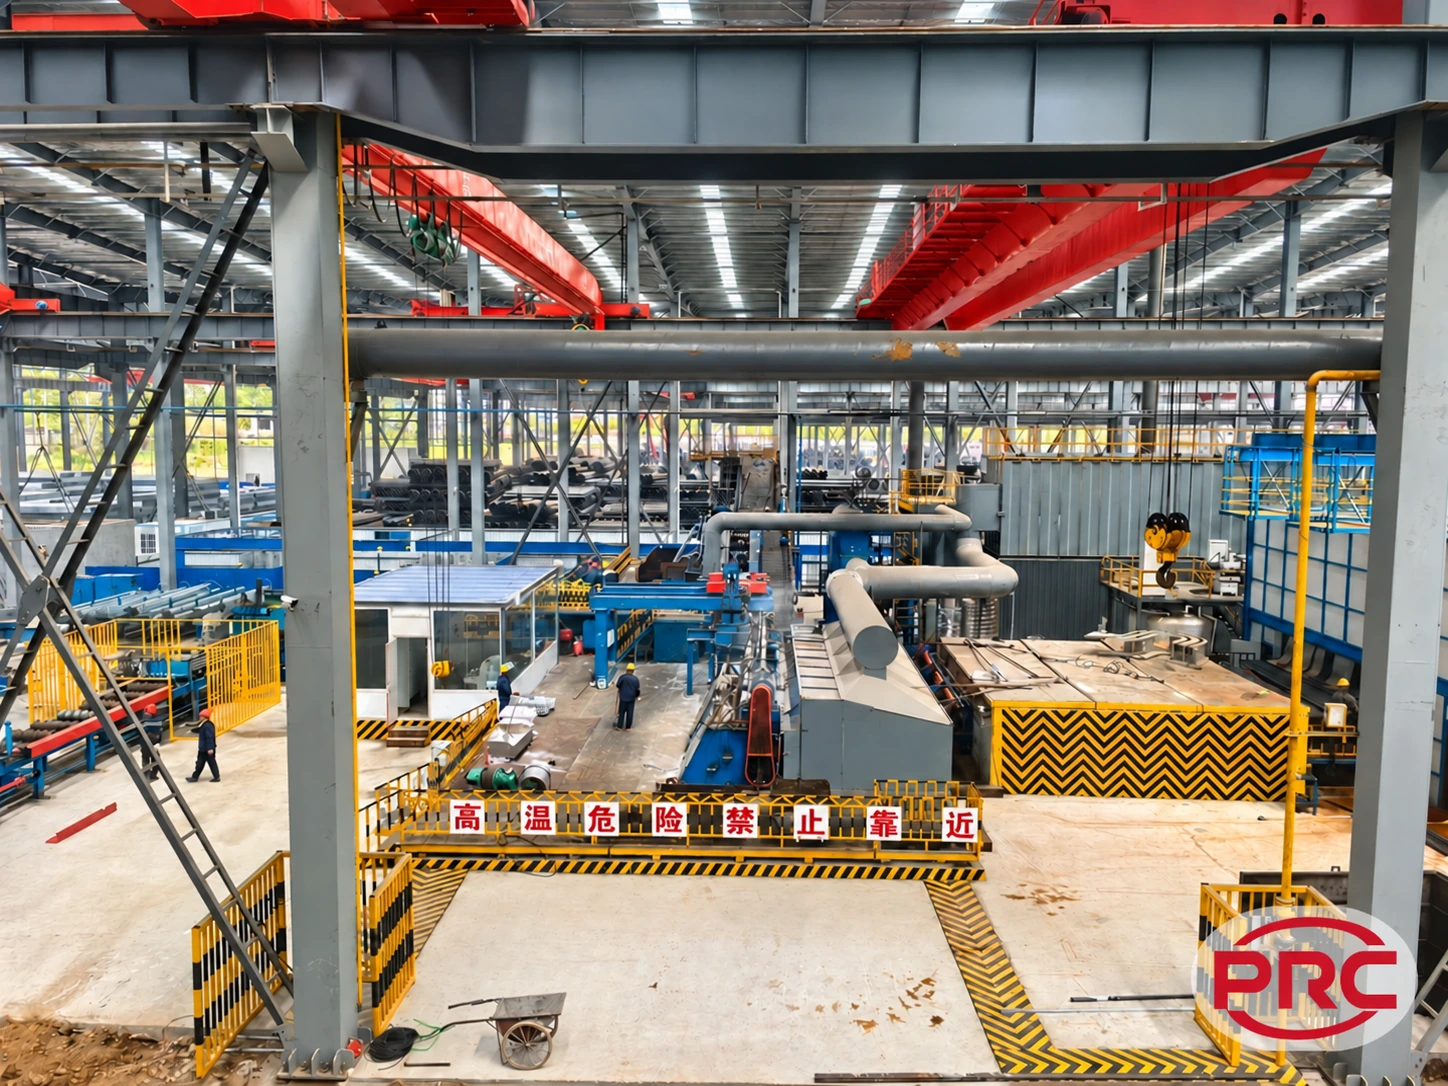
Immerses surface-prepared black steel pipes in molten zinc to coat both internal and external surfaces. Designed for finished pipes, with a material format and equipment arrangement distinct from continuous strip galvanizing.
Provide the diameter range, wall thickness, pipe length, unit weight and annual output so the equipment size, production cycle and layout can be selected.
Surface preparation → Drying & heating → Zinc immersion → Extraction, lifting & blowing → Cooling & finishing
Quick enquiry questionnaire →Continuous hot-dip and alloy coating of steel strip, covering cleaning, reducing annealing, coating, cooling, temper rolling and tension levelling. Galvanizing, galvalume and zinc-aluminium-magnesium coating require product-specific coating chemistry and equipment configuration.
Strip width 600–1800 mm · Strip thickness 0.15–6.0 mm
Cleaning & surface preparation → Reducing annealing → Hot-dip coating & coating control → Cooling → Temper rolling & tension levelling
Quick enquiry questionnaire →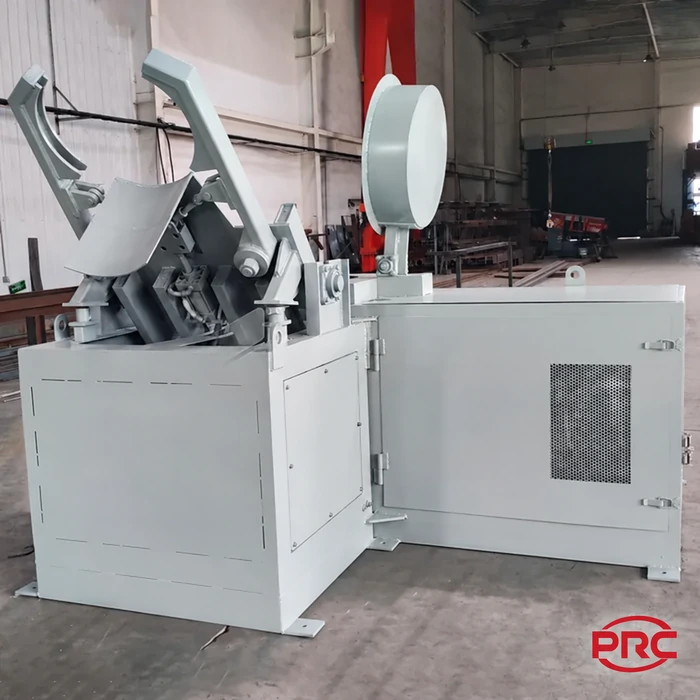
Zinc immersion and centrifugal removal of excess zinc for small metal parts.
View equipmentQuick enquiry questionnaire →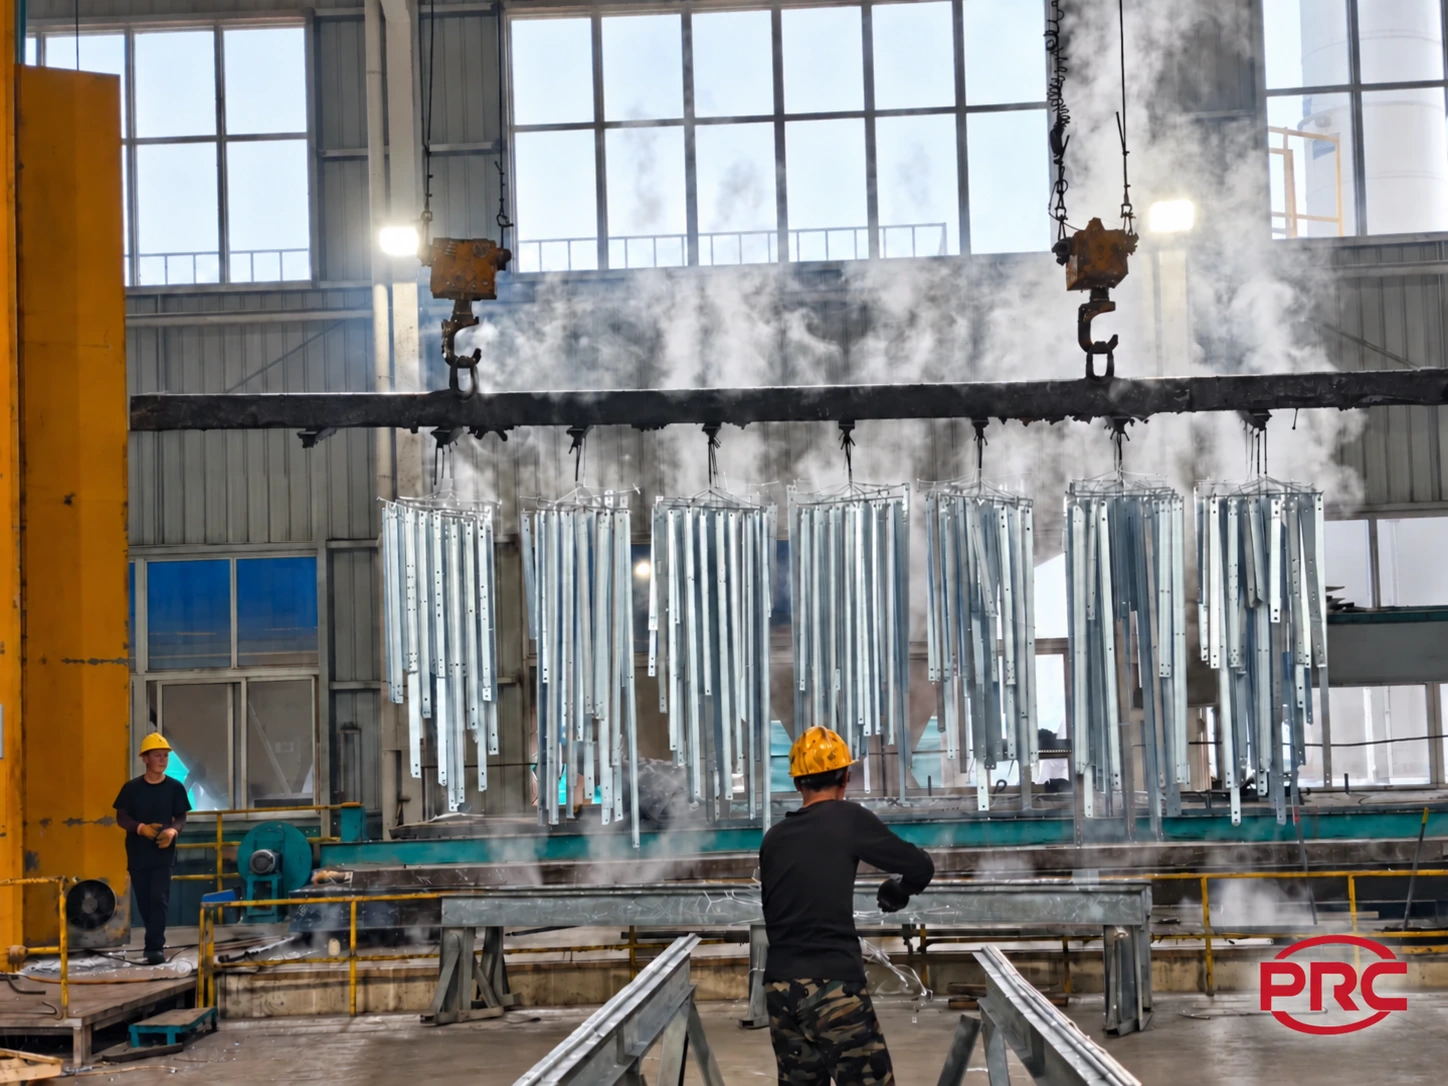
Batch hot dip galvanizing for structural steel and fabricated workpieces.
View equipmentQuick enquiry questionnaire →Pretreatment, zinc coating, cooling and post-treatment of steel wire.
View equipmentQuick enquiry questionnaire →